
Machining cycle
Chamfer and radius on a CNC lathe
A chamfer or radius on any of the four part edges
A clickable cycle form: tap any field to see what it does.
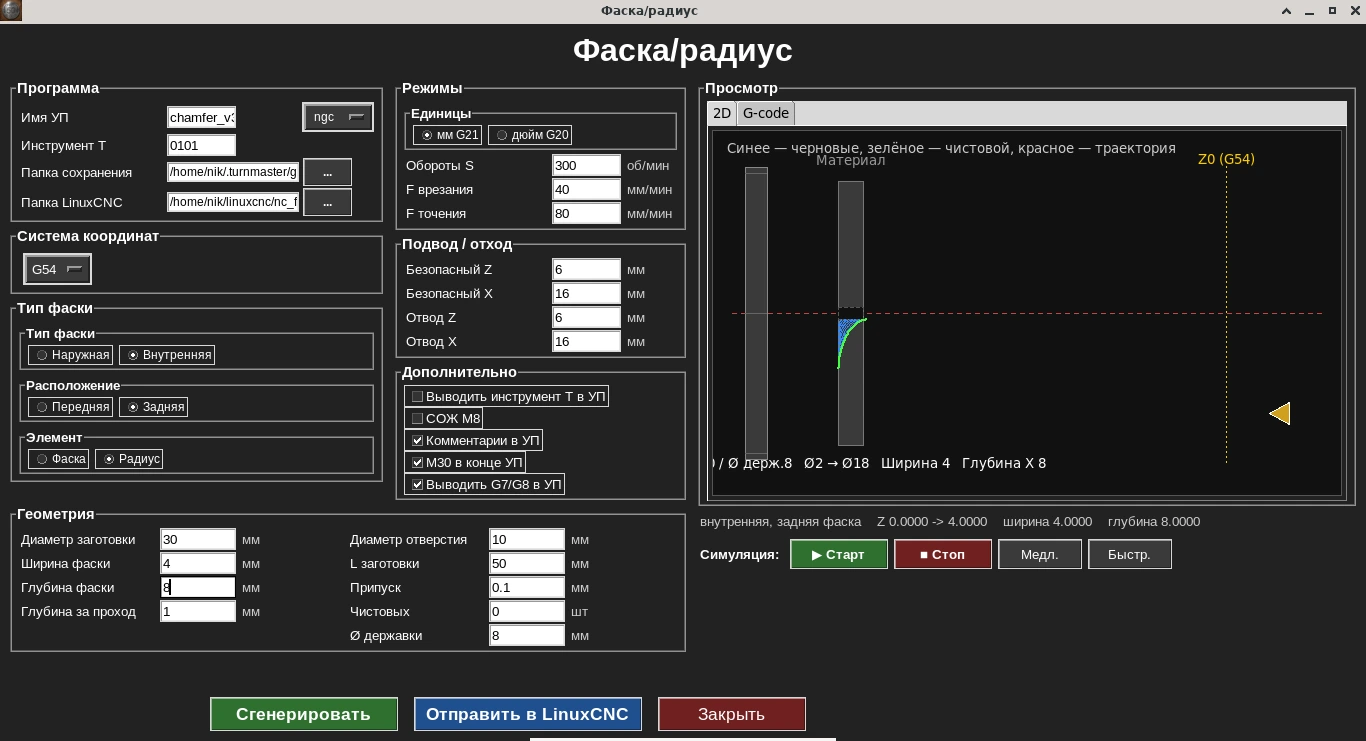
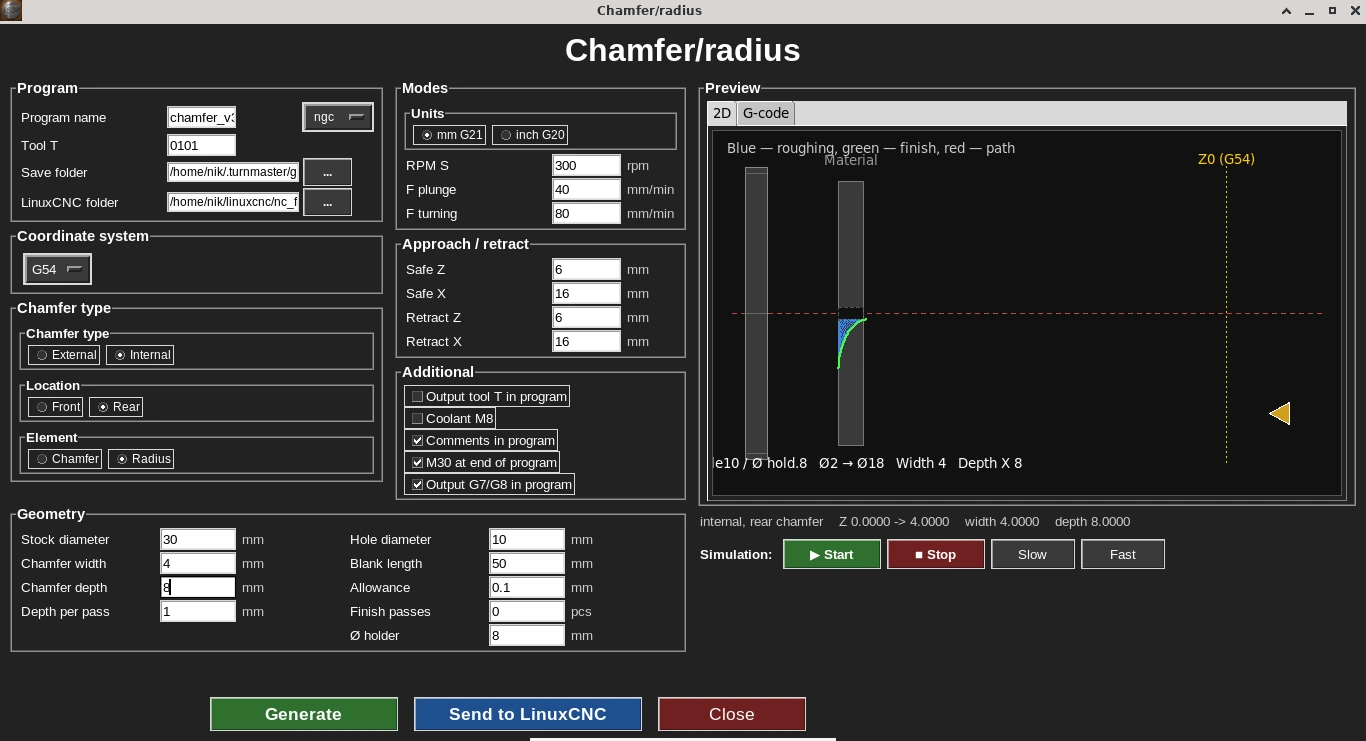
The cycle form: internal rear radius shown — hole diameter, element width and depth, Ø holder, with a live 2D path simulator on the right.
The chamfer/radius cycle machines the selected edge of the part — external or internal, front or back — cutting a chamfer at a given angle or rounding it with a radius.
Who needs this cycle
Needed for rounding or chamfering edges — external and internal, front and back — in all four combinations.
Key form parameters
- •Operation type: chamfer or radius
- •Chamfer size or radius value
- •Edge: external/internal, front/back
- •Feed rate
G-code example
Real output of the Chamfer/Radius cycle in one of its hardest variants — an internal back-side radius: an R4 fillet in a Ø10 mm bore over Z−54…−50. Ø8 mm boring bar, 4 roughing passes of 1 mm, 0.1 mm allowance, plunge 40 mm/min, arc 80 mm/min, 300 rpm. The code lines were not edited by hand.
X in the code is the tool centre, and the edge is further from the axis by the bar radius of 4 mm: the “X to touch: 1.0000” line is the R5 bore wall minus 4. Radius mode G8.
Roughing passes are “self-similar” to the finishing profile: each is the same kind of arc with a smaller radius (R1, R2, R3, R3.9), so the shape grows pass by pass up to the final R4.
chamfer-radius.ngc · 62 lines — Show the full program
%
(Turn G-code)
(Internal radius, back side)
(Bore Ø: 10.0000, bar Ø: 8.0000, X to touch: 1.0000)
(Width Z: 4.0000)
(Depth X/radius: 4.0000)
(Depth per pass: 1.0000)
(Allowance: 0.1000)
(Radius start Z: -54.0000, radius end Z: -50.0000)
(Safe X: 16.0000, Retract X: 16.0000)
(circle R=4.0000)
(Roughing passes are self-similar to the finishing radius profile)

G21 G18 G90 G8 G40 G80 G94
G54

G97 S300 M3
G0 Z6.0000
G0 X16.0000
G0 X0.0000

(Roughing pass 1 of 4: depth 1.0000)
G0 Z-54.0000
G1 X2.0000 F40.0000
G3 X1.0000 Z-53.0000 I0.0000 K1.0000 F80.0000
G0 X0.0000

(Roughing pass 2 of 4: depth 2.0000)
G0 Z-54.0000
G1 X3.0000 F40.0000
G3 X1.0000 Z-52.0000 I0.0000 K2.0000 F80.0000
G0 X0.0000

(Roughing pass 3 of 4: depth 3.0000)
G0 Z-54.0000
G1 X4.0000 F40.0000
G3 X1.0000 Z-51.0000 I0.0000 K3.0000 F80.0000
G0 X0.0000

(Roughing pass 4 of 4: depth 3.9000)
G0 Z-54.0000
G1 X4.9000 F40.0000
G3 X1.0000 Z-50.1000 I0.0000 K3.9000 F80.0000
G0 X0.0000

(Radius finishing pass)
G0 Z-54.0000
G1 X5.0000 F40.0000
G3 X1.0000 Z-50.0000 I0.0000 K4.0000 F80.0000
G0 X0.0000

(Finishing repeat 1 of 1)
G0 Z-54.0000
G1 X5.0000 F40.0000
G3 X1.0000 Z-50.0000 I0.0000 K4.0000 F80.0000
G0 X0.0000

G0 Z6.0000
G0 X16.0000
M5
M30
%
Line-by-line breakdown
G21 G18 G90 G8 G40 G80 G94- Start: millimetres, XZ plane, absolute coordinates, radius mode for X (G8), cancel compensation and canned cycles, feed in mm/min.
G0 Z6.0000 / G0 X16.0000 / G0 X0.0000- Approach: 6 mm in front of the face, then to the part axis — from here the bar travels deep into the bore.
G0 Z-54.0000 → G1 X2.0000 F40.0000- First pass: travel along the axis to Z−54 and plunge in X to X2 — the edge goes 1 mm deeper than the bore wall.
G3 X1.0000 Z-53.0000 I0.0000 K1.0000 F80.0000- A G3 arc of radius 1 back to the bore wall (X1). I0 K1 is the centre offset from the start point: the centre is at X2, Z−53.
G0 X0.0000- Back to the axis before the next pass.
(Roughing pass 4 of 4: depth 3.9000)- Passes 2–4 are the same arcs with radii of 2, 3 and 3.9 mm; the last one leaves 0.1 mm for finishing.
G1 X5.0000 F40.0000 / G3 X1.0000 Z-50.0000 I0.0000 K4.0000 F80.0000- Finishing pass: an R4 arc from X5, Z−54 to X1, Z−50 with its centre at X5, Z−50 — the final radius.
(Finishing repeat 1 of 1)- A repeat of the finishing pass on the same path — it cleans up whatever may be left by the boring bar springing.
G0 Z6.0000 / G0 X16.0000 / M5 / M30- Exit the bore, retract, spindle stop and program end.
Comments in this program were translated from Russian; the G-code itself is unchanged.
What the codes in this program mean (G0, G1, G3, G8, M3, M5) — G- and M-code reference for lathes.
Frequently asked questions
How many edge combinations does the cycle support?
All four — external front, external rear, internal front, internal rear.
Can I choose between a chamfer and a radius?
Yes, the operation type is a separate parameter — an angled chamfer of a given size, or a rounded edge of a given radius.
Do I need a separate pass for each edge?
Yes, each edge-and-operation-type combination runs its own cycle calculation, so you control exactly where the chamfer or radius is cut.
Can I preview the result before generating the G-code?
Yes, the cycle form shows a live 2D toolpath simulator for the selected edge.