
Free Turn G-code demo
Online CNC lathe G-code generator
The OD turning cycle right in your browser: enter the diameters, length and cutting data, and the generator works out the roughing passes, the finishing pass with allowance and writes a ready program for LinuxCNC. It is the same calculation as in the Turn G-code program, line for line. No sign-up.
Preview
G-code
This is one cycle out of 12
The program has 11 more, including multi-start and tapered threads with run-in and run-out, sphere and a face spiral. It runs on the machine PC itself, offline, and is set up for your control.
Download the program — 15 days freeThen $99 lifetime, no subscription
Download later, on the PC at your machine?
We'll email you the trial link. It's optional — you can download the program without an email.
One email with the link and, if you don't download, up to 3 short reminders. No newsletters.
All 12 cycles in the program
Only OD turning runs in the browser. In the program on your own computer all 12 cycles run, each with its own form and 2D simulator. On each cycle page you can click through its form in the interactive help.
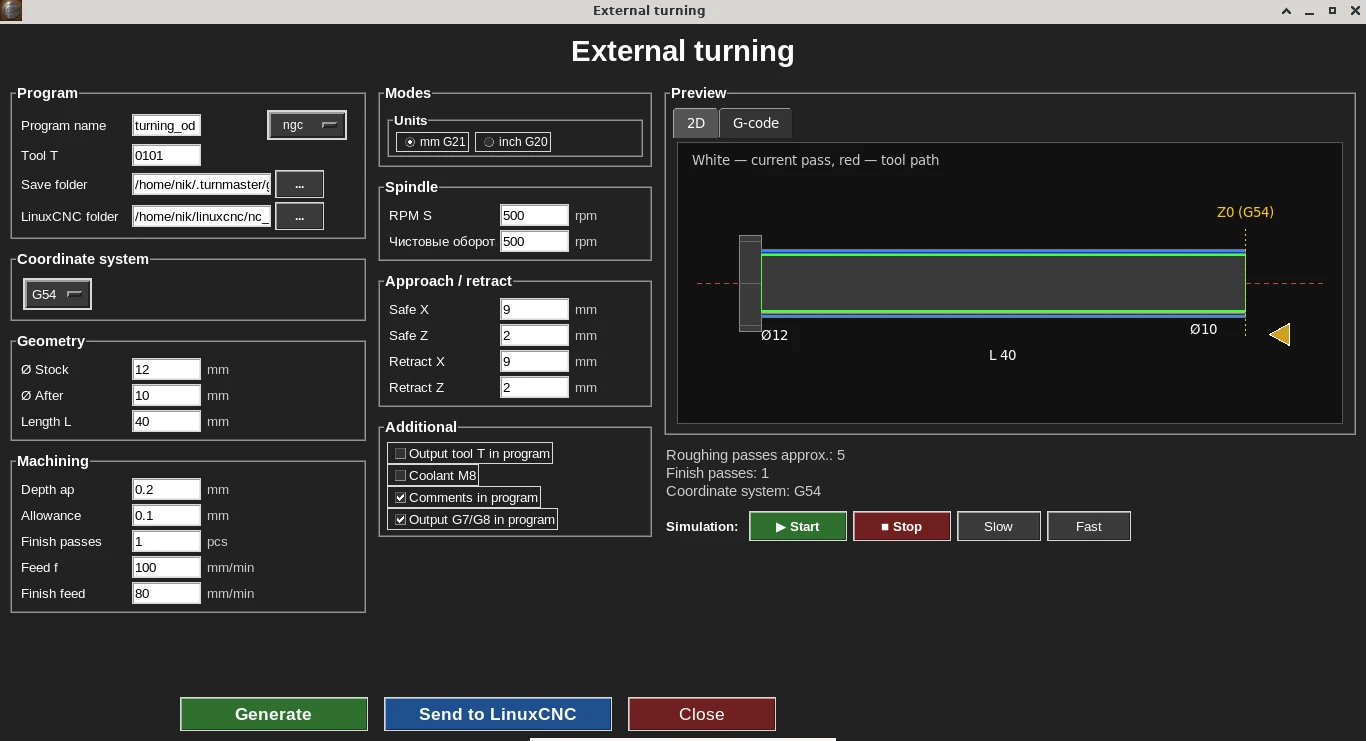
Turning
The core roughing and finishing cycle for outer-diameter turning
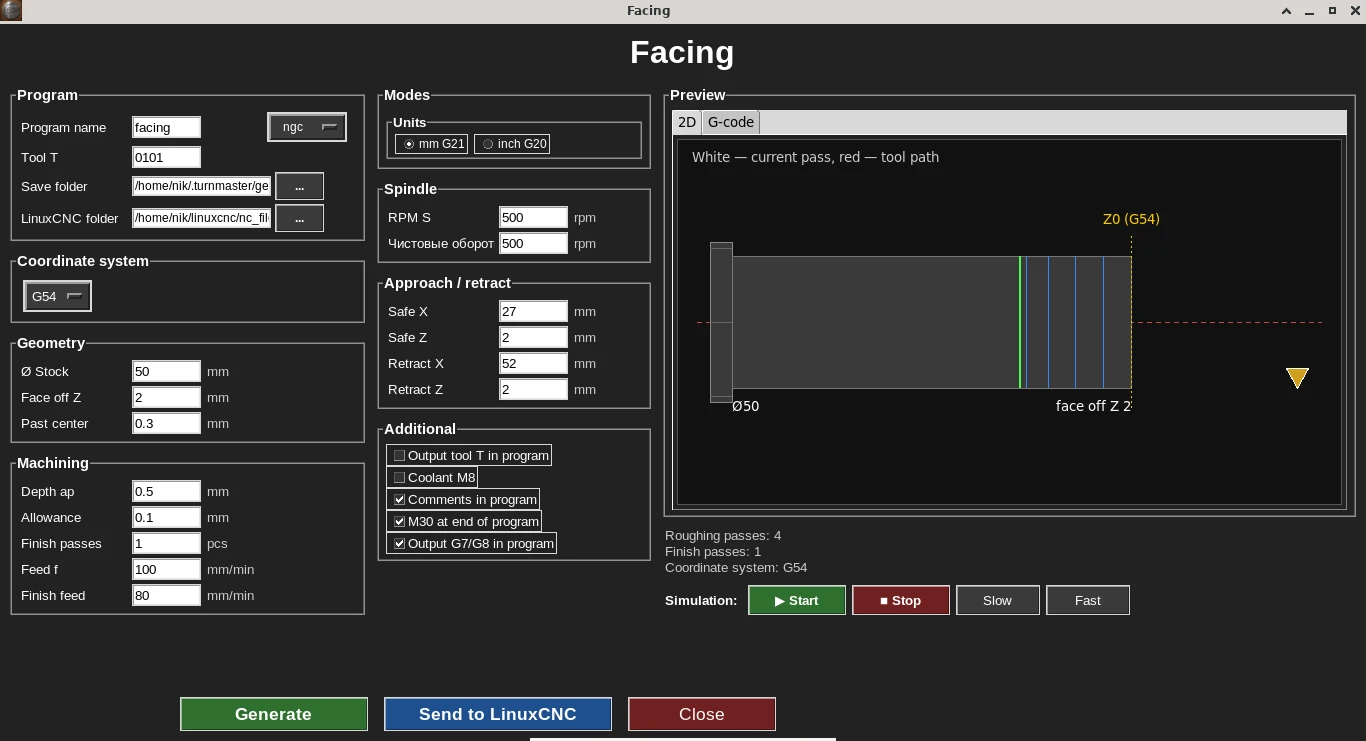
Facing
Machining the face of a workpiece down to the required length
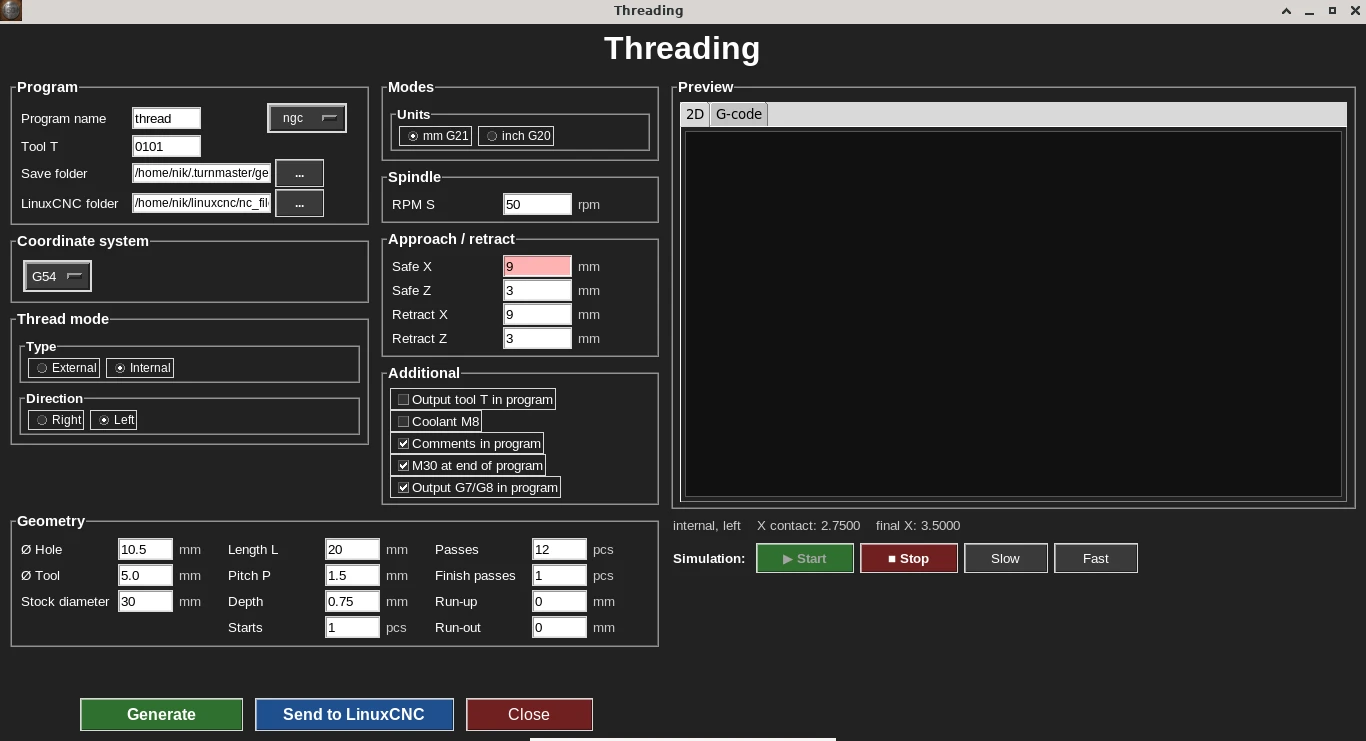
Threading
External and internal threads: right/left-hand, multi-start, with lead-in and lead-out
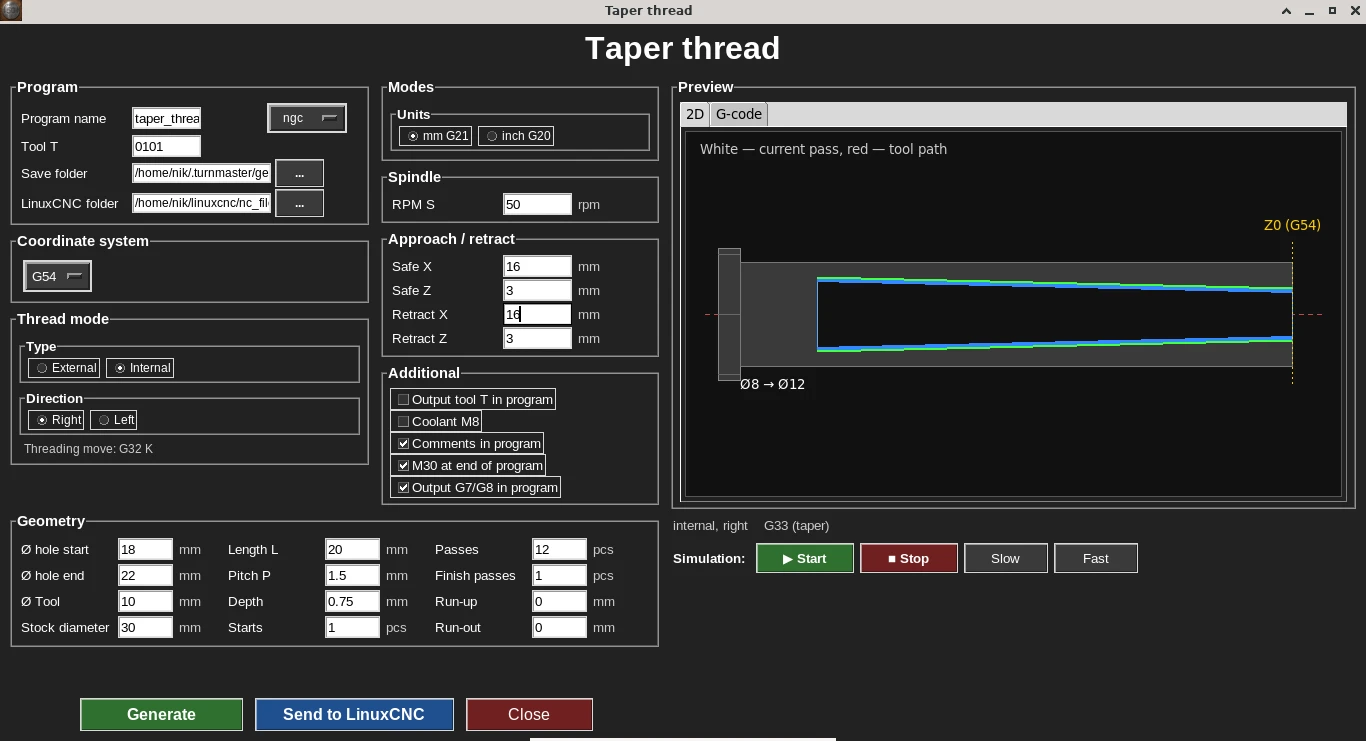
Taper threading
The same threading capability, applied to a tapered surface
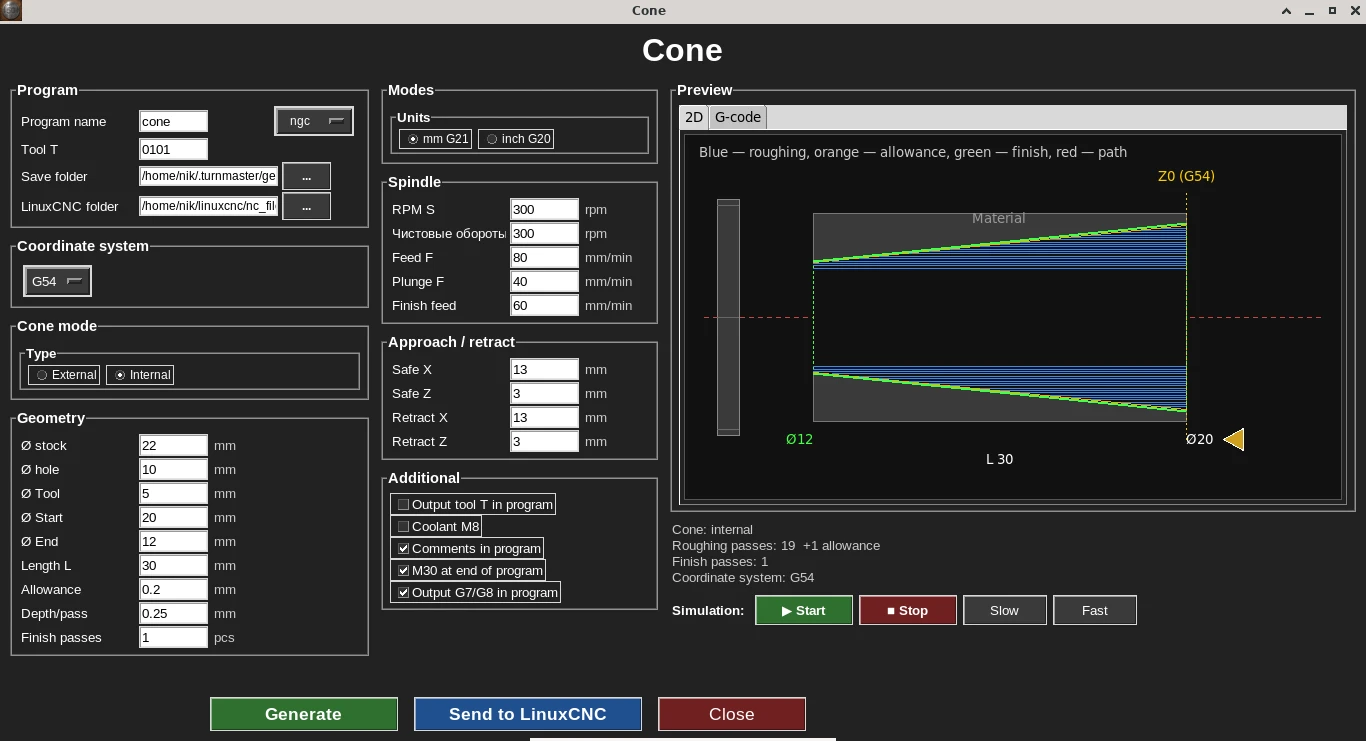
Taper
External and internal conical machining
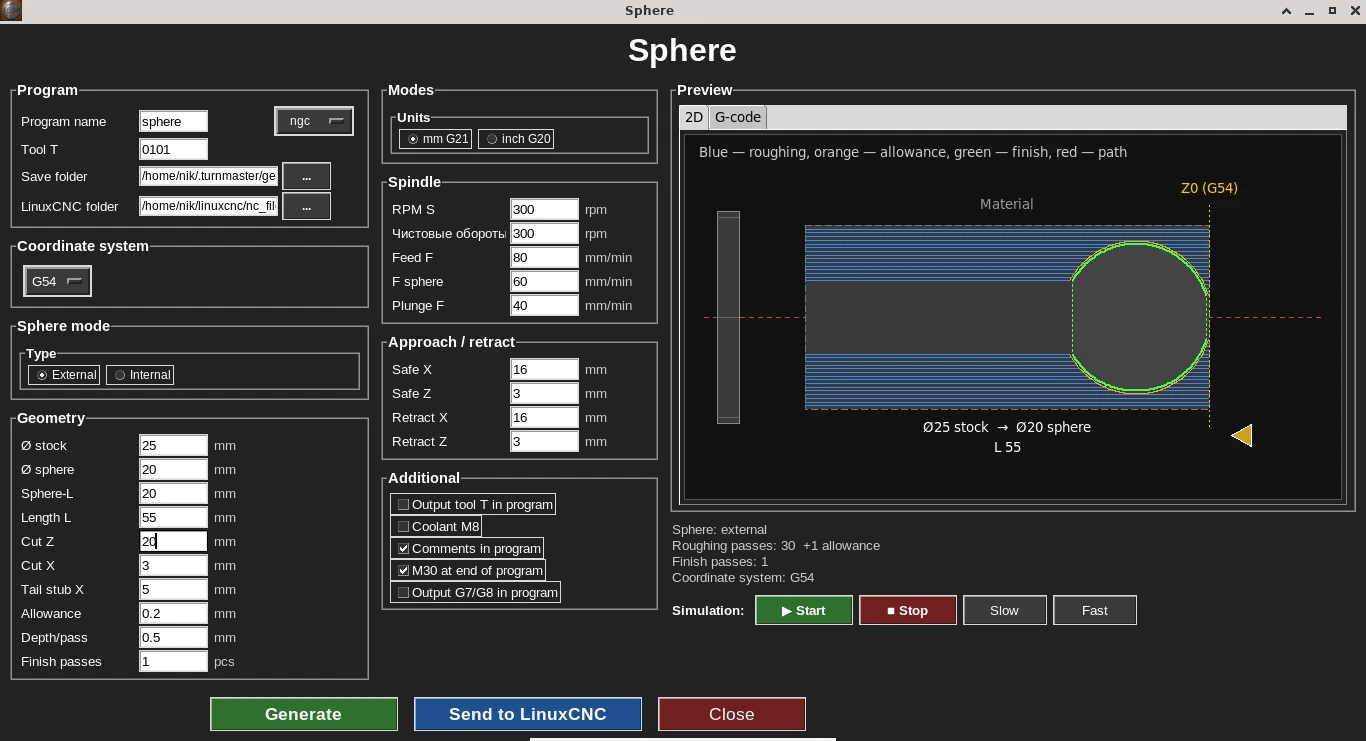
Sphere
Spherical and concave profiles, including grooved pulley profiles
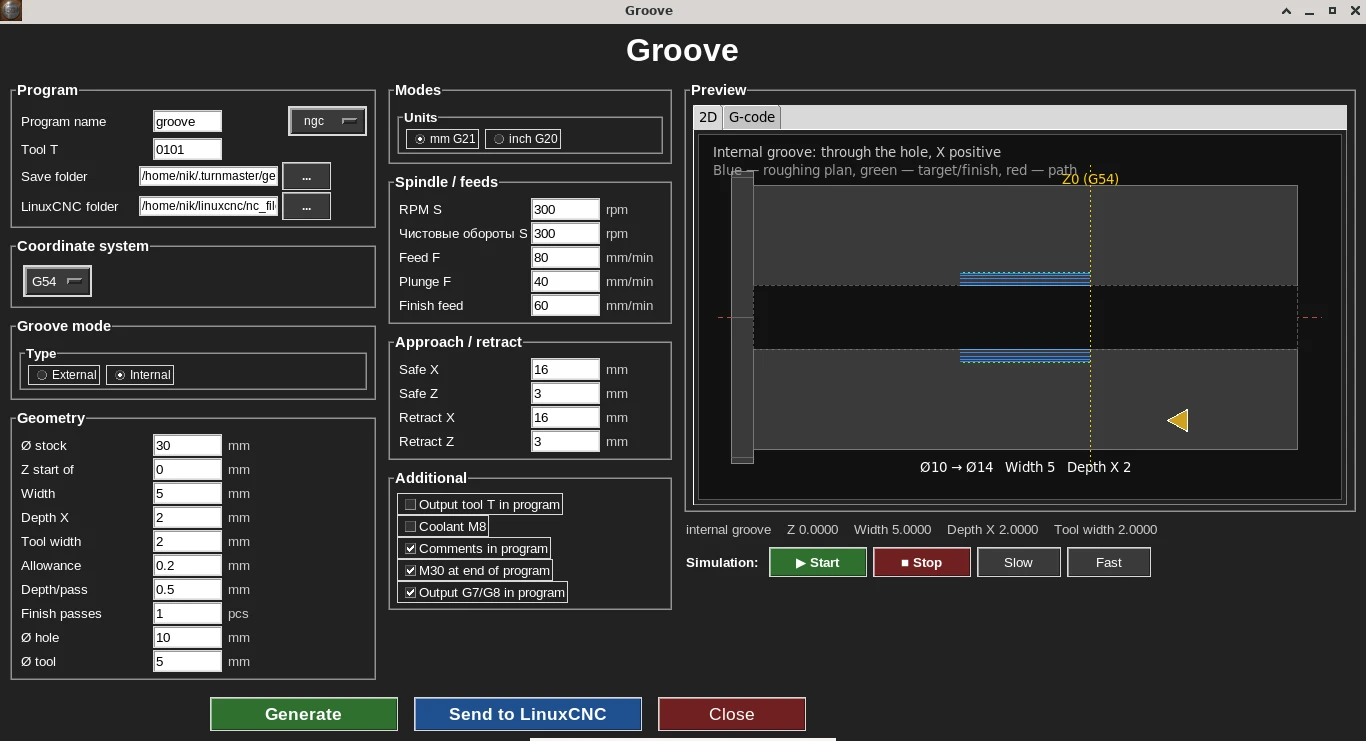
Groove
Cutting grooves of a given width and depth
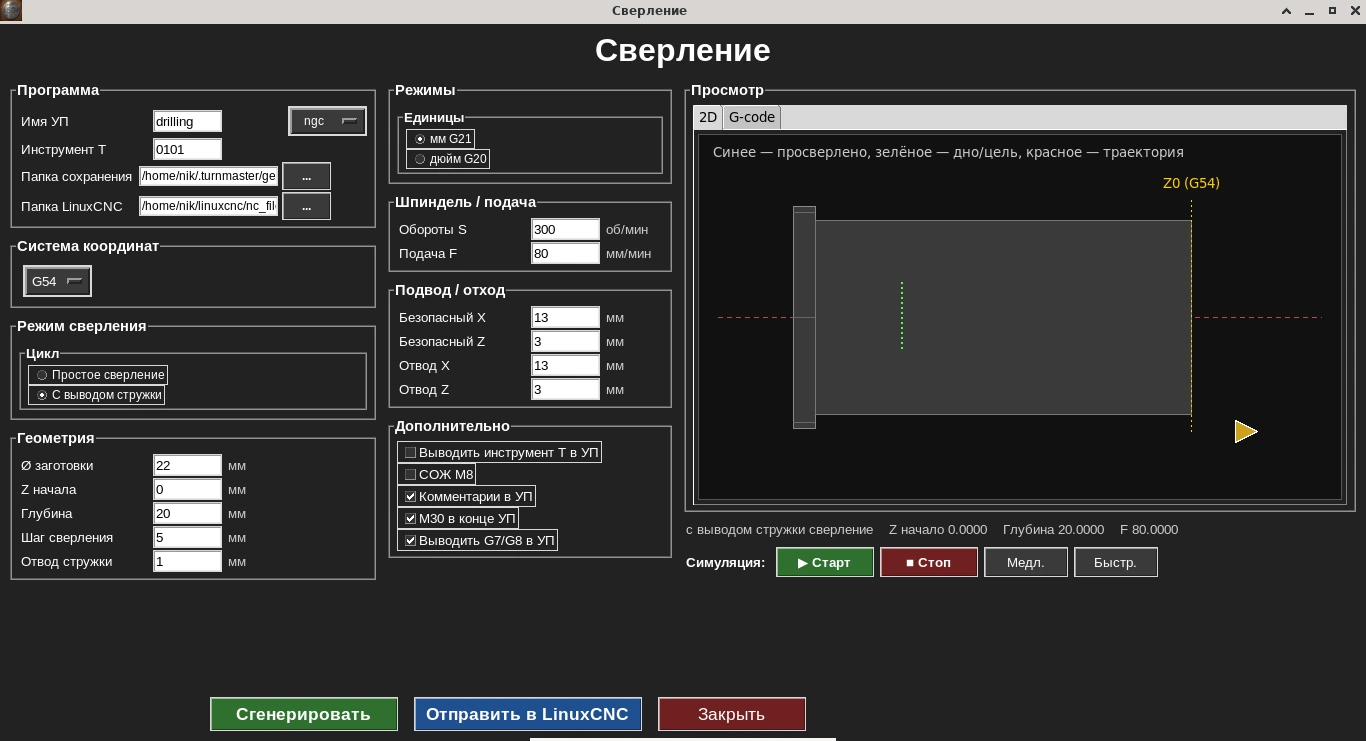
Drilling
Axial drilling with support for peck feeding
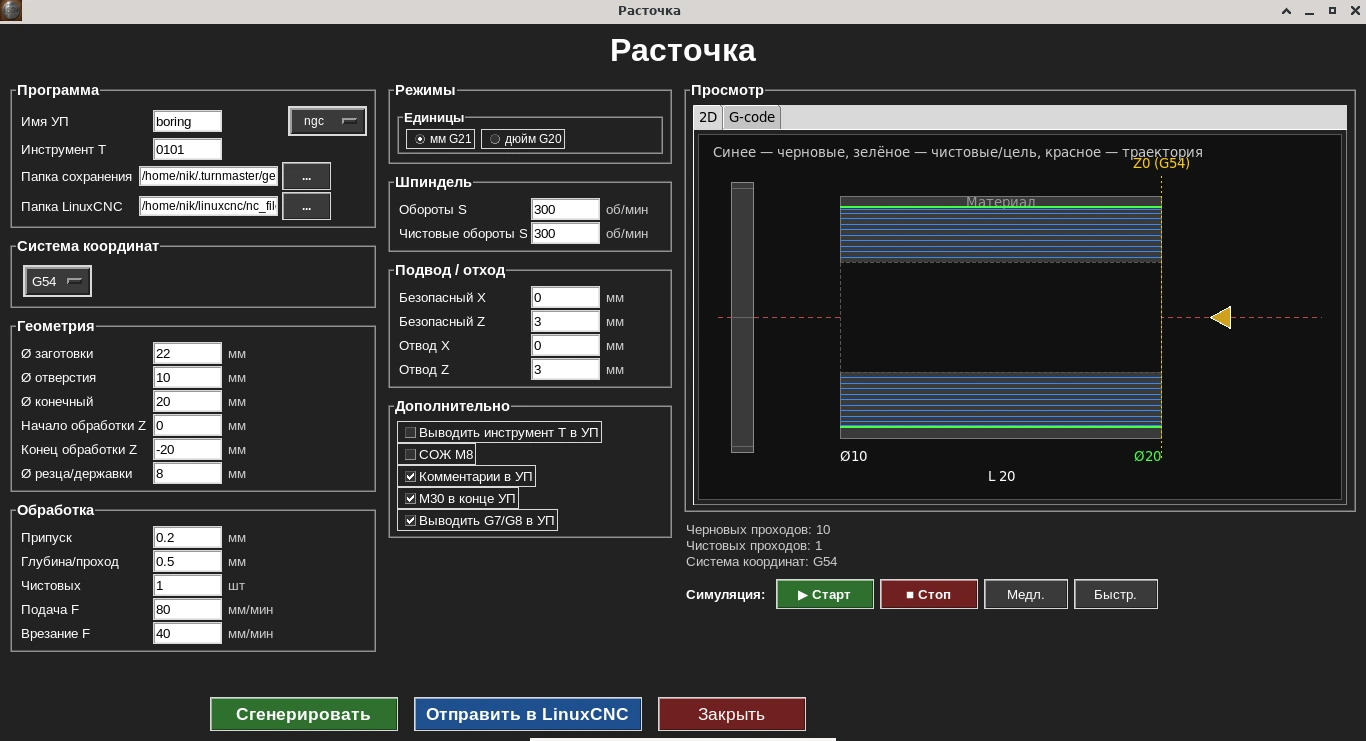
Boring
Boring internal diameters
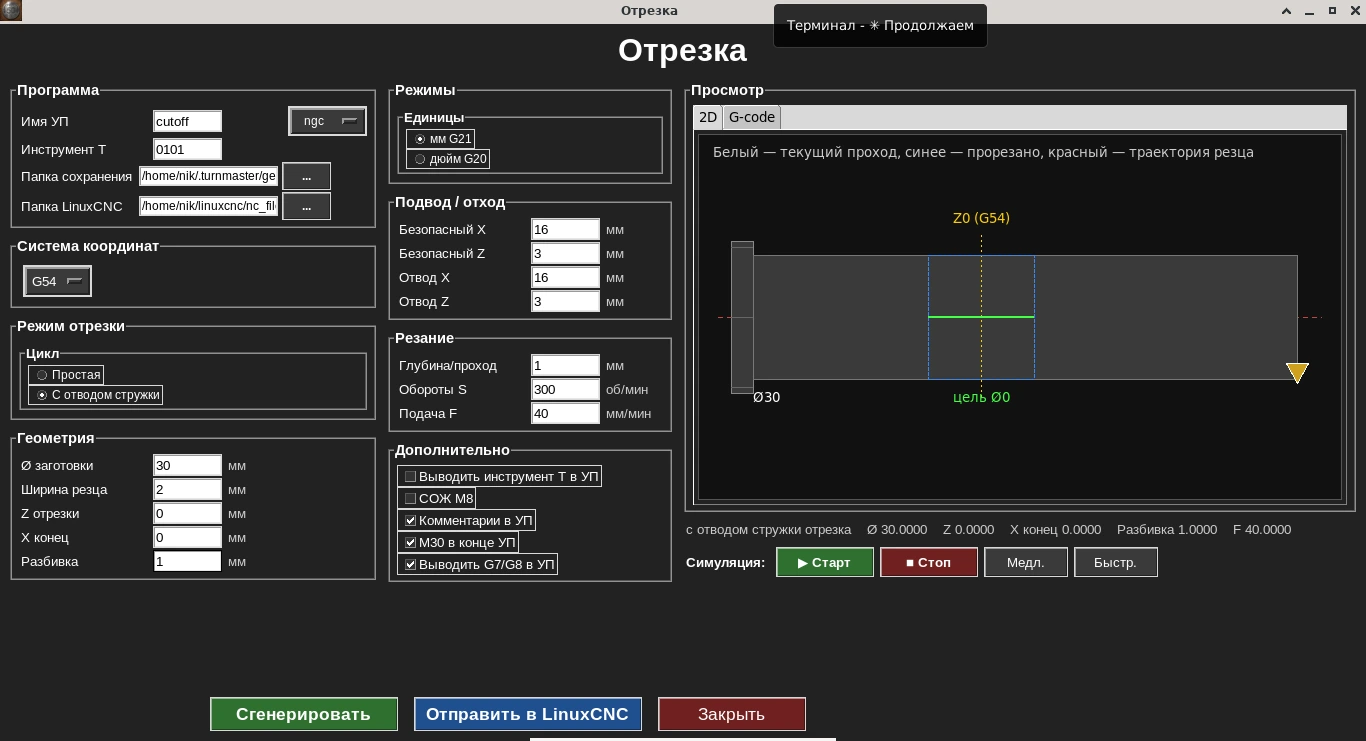
Cutoff
Parting off the finished part from the stock
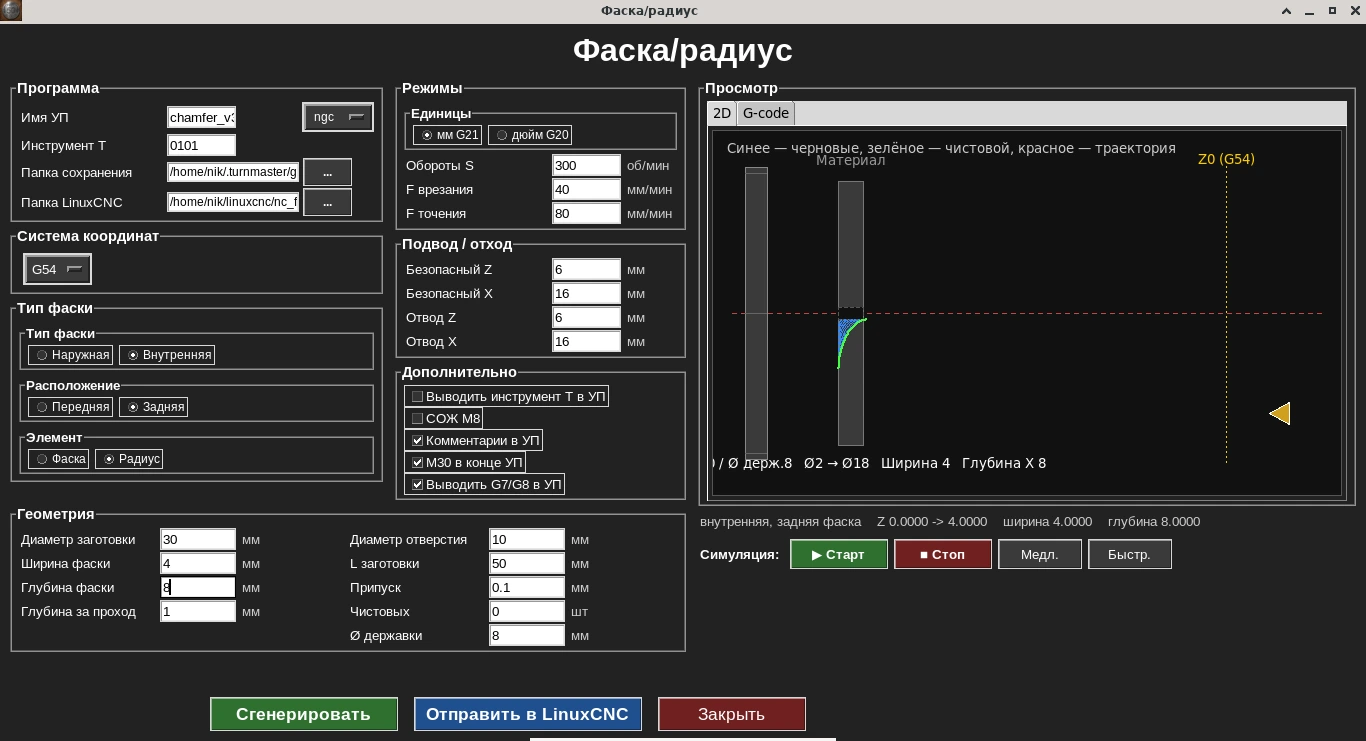
Chamfer / radius
A chamfer or radius on any of the four part edges
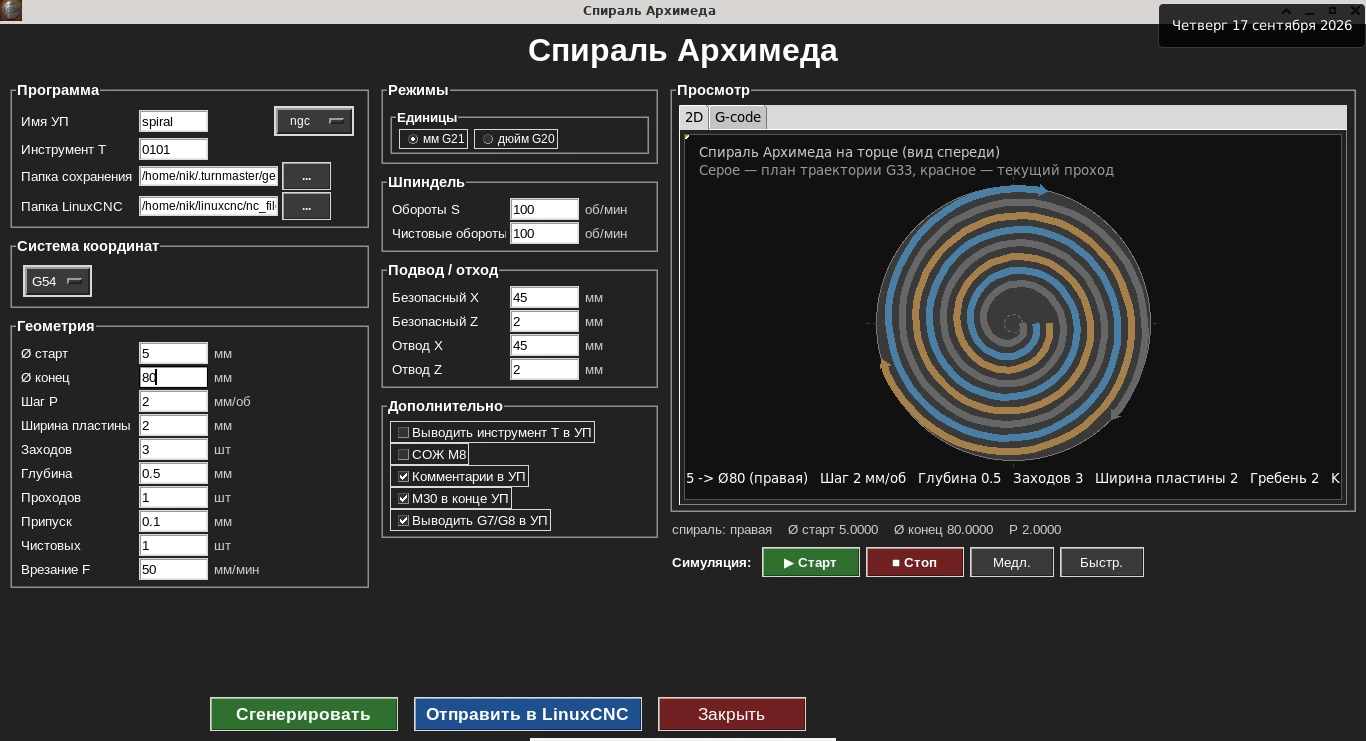
Archimedean spiral
A face spiral thread/groove following the Archimedean spiral
How to use it
- Geometry: stock diameter, finished diameter and the length from the face (Z0) to the left.
- Machining: roughing depth per side (ap), finishing allowance, number of finish passes and feeds in mm/min.
- Approach / retract: the safe X and Z the tool starts each pass from, and the retract point at the end. X is entered as a radius and must not be less than the stock radius (with G7 the code shows it as a diameter).
- Check the toolpath in the 2D view or press "Simulate", then copy the code or download the file (.ngc, .nc or .tap) and open it in LinuxCNC. Before the first cut, check the LinuxCNC preview and run it in the air.
FAQ
Is it free? Yes, the online turning generator is free with no sign-up. The Turn G-code program with all 12 cycles is free for 15 days, then $99 lifetime.
Is the code the same as in the program? Yes, it is the same calculation; only a comment line about the web demo is added at the top.
Which control is the code for? The demo writes code for LinuxCNC (G7 or G8, mm, G94). For other controls — grblHAL, PathPilot, Fanuc System B/C — the settings are in the program; see Which CNC controls Turn G-code works with.
Why no threading? Threading, taper, sphere, grooves and the other cycles are in the program. How the whole generator works is in CNC lathe G-code generator.